To validate an OCA lamination process, test samples that reflect the actual display stack—not simply a panel that happens to bond well. A clear-looking sample is a start, but the more useful question is whether that result holds when the materials, geometry and processing conditions resemble production. Representative samples, traceable trial conditions and consistent inspection help separate an encouraging first run from a process that can be repeated.
What Does a Successful Lamination Trial Really Prove?
A panel can leave the laminator looking clear and properly aligned, yet say little about the next build. Change the cover material, adhesive or supporting fixture, and the same machine recipe may behave differently. A useful trial answers a defined engineering question rather than simply producing a presentable sample.
For an industrial display project, that question has several parts: will the intended surfaces bond with the selected OCA, can the equipment reproduce the important conditions, and does the result hold across the production variation that matters? These are related concerns, but a pass on one does not settle the others.
Take a single panel that passes visual inspection. It supports initial feasibility for that particular stack and cycle. It says little about a thinner cover, another adhesive lot or a more difficult edge geometry unless those conditions were part of the trial.
The result is only as broad as the trial. State which display structure, adhesive, bonding interfaces and conditions were evaluated, and which inspection criteria were applied. Anything outside that scope remains a question for further testing.
This is where process validation and equipment acceptance part ways. A factory acceptance test can show that a machine meets agreed functional requirements. It cannot, by itself, prove that a particular OCA will bond the intended display stack; that takes material-based trials.
Keeping those questions separate helps avoid a costly mismatch: a machine may perform its specified cycle correctly while the display still needs different tooling, handling or process conditions.
Which Samples Are Close Enough to Production to Matter?
The easiest material to test is not always the best stand-in for the finished display. A flat surrogate may show whether a fixture holds a panel securely, but its surface, stiffness and layer arrangement may tell you little about bonding the actual stack. The closer the trial gets to the production interface, the more meaningful its result becomes.
The baseline is the intended LCD or OLED construction: cover material, OCA specification, layer thicknesses, bonding surfaces and relevant edge details. These are more than drawing references. Each can affect contact, alignment or support during pressing.
Then look at how the product range differs. Two panel sizes may present much the same bonding challenge, while two stacks with similar outside dimensions may behave differently because one includes a flexible layer. Samples are most useful when grouped by changes that affect the process, not by product names alone.
| Sample role | What it establishes | What remains unconfirmed |
|---|---|---|
| Production sample | How the intended material stack behaves under the proposed bonding conditions. | Performance across every material or dimensional variation. |
| Boundary sample | How a selected demanding combination of geometry, thickness or substrate characteristics affects the process. | Other boundary conditions that have not been included in the trial. |
| Surrogate sample | Preliminary equipment handling, fixture positioning or platform arrangement. | Final bonding compatibility and optical quality of the production stack. |
The hardest sample is not necessarily the largest panel. A flexible substrate can challenge mechanical support; a printed border, cutout or different layer geometry can affect local contact. A boundary sample earns its place because it probes a plausible weakness in the process, not because it looks extreme on paper.
Lot records become particularly useful when results disagree. If a later panel shows bubbles or edge defects, knowing whether the OCA batch, storage history or cover material changed helps narrow the investigation before anyone starts adjusting the recipe.
Adhesive choice belongs in that comparison as well. Different adhesive forms and supplier-defined constructions may call for different handling and bonding routes. JiuTu’s article on adhesive form and process compatibility explains why these routes should not be treated as interchangeable.
Once the relevant stack variations are clear, the OCA vacuum laminating machines can be considered in terms of the platform, tooling and process controls the trial actually needs, rather than compared only by published features.
How Do You Know What Changed the Result?
When a sample fails, the machine recipe is not necessarily the cause. Adhesive condition, the way the panel sits in its fixture and small changes at the bonding interface can affect the outcome. A useful trial record therefore connects the inspection result to the actual panel that went through the machine.
Each sample needs an identity that follows it from preparation through any follow-up checks. Drawing revision, OCA lot and fixture configuration matter as much as the recipe; without them, two runs may look comparable on paper when they are not.
Suppose the vacuum setting and the OCA lot both change between two runs. If the second panel looks better, there is no clear way to tell which change helped. When investigating a setting, keep other influential factors as stable as practical and record any deviations.
Keep the result tied to the sample
A compact record keeps the essential details together:
Visual quality needs context. Bubbles, misalignment, incomplete contact, edge conditions, contamination or optical nonuniformity may all matter, but different displays can have different acceptance limits. The specification should decide what counts as a defect, not a generic judgment that the panel “looks clear.”
Even two sound inspections are hard to compare if the panels were viewed under different lighting or at different stages. Use consistent viewing conditions and link photographs of any defect to the sample identification and inspection result.
Some OCA systems need more than the first bonding cycle before the result can be judged. Depending on supplier instructions and display construction, the sequence may include film application, vacuum lamination, bubble removal or autoclave treatment. Inspect after the stages the selected process actually requires; a panel that looks clear immediately after pressing may not be the final result.
The adhesive supplier’s technical documentation should guide material limits. A recipe carried over from a different stack or machine is a starting hypothesis, not a confirmed setting. JiuTu’s technical FAQ offers related context, but the selected materials still need their own trial evidence.
When Does a Good Sample Become a Repeatable Process?
The useful shift comes when the team can explain not just why a panel passed, but how reliably the same result can be obtained. That requires repeat trials within a defined range, rather than extrapolation from the cleanest sample. Even consistent trial results do not automatically complete production qualification; reliability testing and production variation may still need separate review.
There is no universal sample count that makes every process ready for production. The amount of repetition depends on the risk, the display application and the acceptance agreement. A trial for a single fixed stack will not necessarily need the same evidence as a line expected to handle several variants.
Those repeated results need criteria agreed before the runs: alignment tolerance, visible defect limits, edge quality and any application-specific optical checks. Choosing the limits after seeing the panels may make a recipe easier to approve, but it makes the conclusion much less useful.
Conditions supported by trial results
The specified material stack has been processed under documented conditions, repeated results have been reviewed, and inspection findings meet the agreed criteria within the evaluated range.
Conditions outside the tested range
Different adhesive specifications, untested thickness combinations, revised tooling or operating conditions that were not included in the trial should not inherit the same validation status automatically.
A process window is the range of conditions that has held up in testing, not a single recipe that produced the best-looking panel. If acceptable results appear only at one narrowly controlled setting, normal differences in materials or handling may expose a weak margin.
This is where machine selection becomes specific. A stack sensitive to pressing force or displacement raises one control question; a sequence that needs several pressure stages raises another. Fixture support and vacuum conditions may matter just as much as the headline machine rating.
JiuTu’s servo and staged pneumatic configurations illustrate two different approaches to those questions.
How the Equipment Choice Follows the Trial
Neither configuration replaces a sample trial. The useful comparison is which process variable the equipment can control for the display being evaluated.
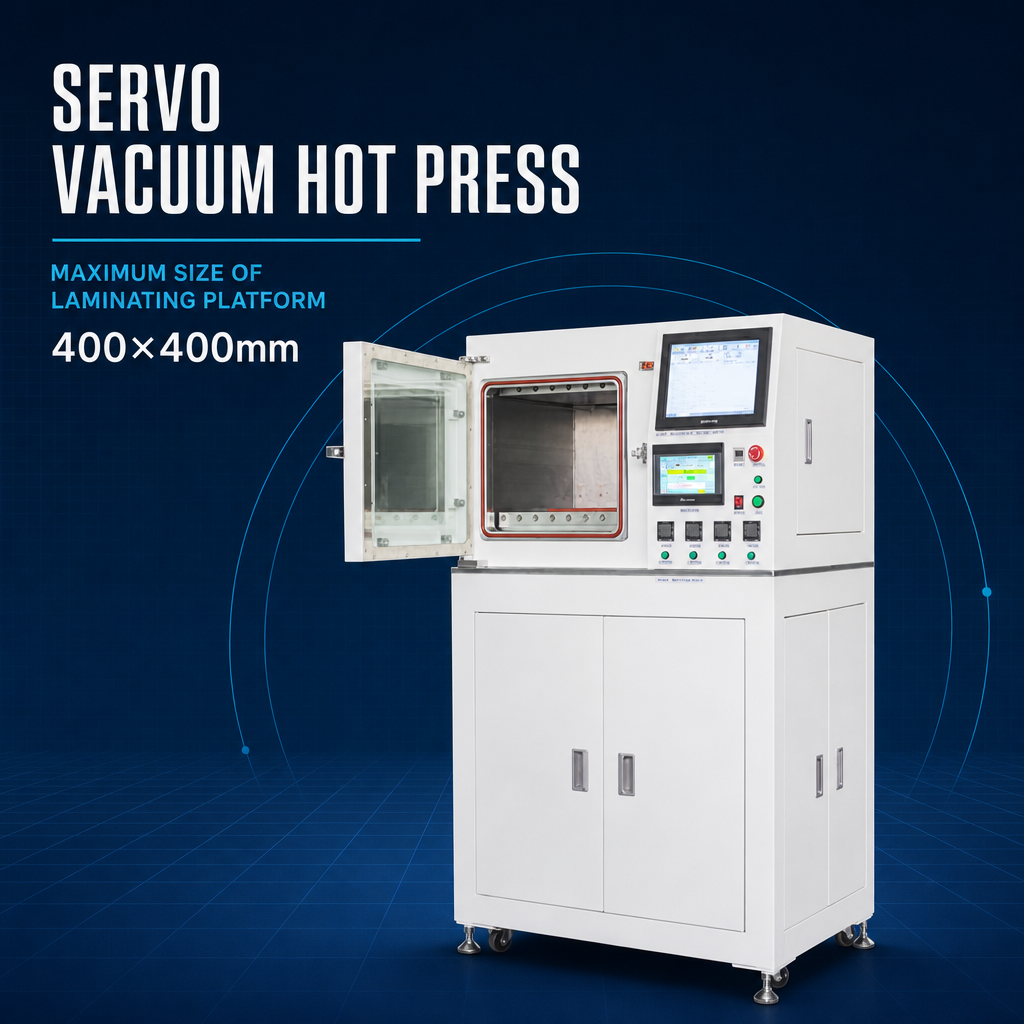
Servo Pressing Configuration
400×400-2T Servo Laminating Machine
Where the trial needs to examine how pressing force relates to displacement and motion, the 9TU-M040E’s servo configuration provides a relevant option. Its vacuum and non-vacuum modes also need to be assessed against the intended bonding sequence.
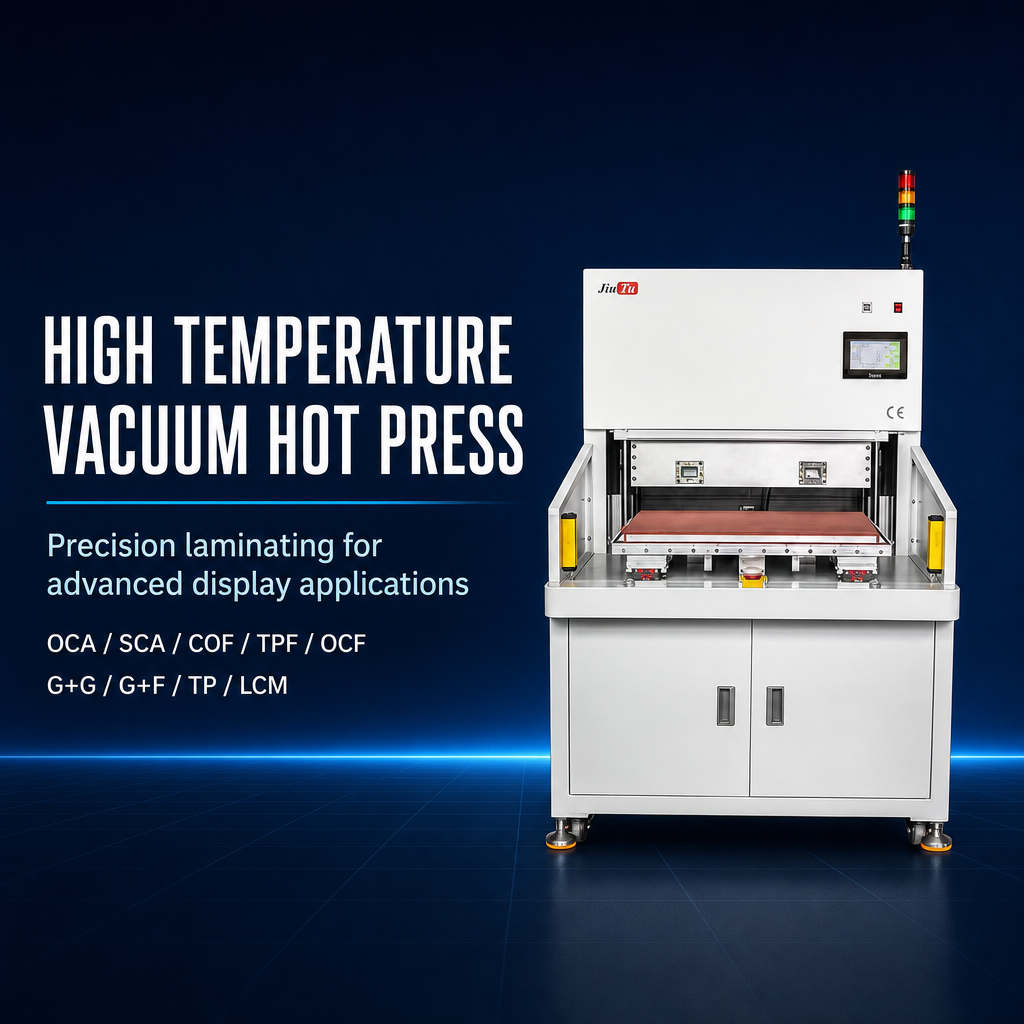
Staged Pneumatic Pressing
9TU-M040D Industrial Vacuum Laminating Machine
If the bonding sequence calls for different pressure conditions across successive stages, the 9TU-M040D offers a staged pneumatic approach with configurable recipes. The question is whether that sequence suits the actual interfaces and fixture, not simply whether the machine can store the settings.
Neither pressing approach is inherently right for every display. The stronger choice is the one whose controls and tooling can reproduce the conditions demonstrated by the representative samples.
Which Changes Make the Original Trial Less Useful?
A validation result becomes less useful when the product or process no longer resembles what was tested. The question is not simply whether a drawing or material code changed, but whether that change can alter adhesive contact, mechanical support or the way the bonding cycle is applied.
Switching the OCA construction, supplier or thickness may change handling and bonding requirements. A different cover material or surface treatment can be just as consequential, even if the panel dimensions remain the same.
Geometry can change the answer too. A new cutout, curved edge or unsupported area may alter how the stack sits in its fixture and where pressure reaches the interface. A display that looks similar on a drawing may still need its own assessment.
A revised fixture, pressing arrangement or vacuum sequence is another reason to look again. What matters is whether the change moves the process beyond the conditions supported by the original trials.
A new material lot does not automatically mean starting over. If it meets the approved specification and the relevant variation is already covered, documented verification may be enough. Supplier information and the project’s change-control rules should determine the scope.
The same reasoning applies when defects appear after previously acceptable runs. New bubbles, edge separation or alignment drift call for a comparison with earlier samples before adjusting the recipe. The cause may be upstream of the laminator.
Sometimes that comparison points to a limited verification; other times it shows that a different material stack or pressing method needs a broader trial. The scope follows the technical impact of the change, not a blanket rule that every revision requires full revalidation.
Frequently Asked Questions
Is one successful sample sufficient to validate an OCA lamination process?
No. It shows that one material stack can bond under one set of conditions. Repeatability and the acceptable process range require broader evidence, with inspection criteria agreed in advance.
Can a surrogate substrate be used for an OCA bonding trial?
Yes, for early handling or fixture checks. But if its surface, stiffness, thickness or construction differs from production, it cannot establish the final bonding quality of the intended stack.
What changes require another validation trial?
Changes that affect adhesive contact, mechanical support, tooling or critical process conditions may call for further trials. A variation already covered by the evaluation may need only documented verification; a materially different stack may require more.
OCA Process & Equipment Evaluation
Bring the Actual Display Stack Into the Equipment Discussion
When the sample results begin to reveal which conditions matter most, equipment discussions become more productive. The goal is to work out what a proposed laminator needs to reproduce and what remains to be tested.
A useful starting point for that discussion includes:
- Display type, dimensions and complete layer stack
- OCA supplier, material code and technical data sheet
- Fixture drawings, bonding sequence and process conditions
- Representative samples, inspection criteria and known defects
These details help focus the review on a real bonding problem rather than a generic machine specification. Final suitability still depends on trials with the intended materials and tooling.