Before an optical bonding machine leaves the factory, the FAT should establish that the delivered configuration matches the approved specification, its essential functions have been demonstrated, and any shipment-blocking issues have been resolved.
That takes more than a successful cycle on a touchscreen. The factory acceptance test needs agreed pass conditions, representative samples where required, credible measurements and an acceptance record that makes outstanding work visible. It is a decision about whether the equipment is ready to ship—not a promise of production yield once it reaches the plant.
Start With the Agreed Acceptance Scope
A factory demonstration can feel reassuring: the press moves, the controls respond, and the test piece comes out. Yet none of those observations settles the purchasing question unless the team knows what the machine was contracted to do. A smooth demonstration of an unagreed setting has little bearing on a missing option or an untested requirement.
The approved specification should therefore lead the discussion. It identifies the configuration being delivered, the functions that matter to the project and the conditions under which each one can be accepted. That includes such details as the ordered tooling, usable working area, pressing method, applicable heating or vacuum controls, recipe functions and required protective devices. Only the features included in the contract should be treated as acceptance obligations.
Before the first operating cycle, verify that the machine itself matches the order. Check the model and unit identification, supplied options, tooling and key dimensions against the purchase specification and approved drawings. Record visible damage or missing items, and confirm that manuals and drawings included in the supplier’s scope are available. This establishes that the unit being tested is the configuration the buyer agreed to purchase.
Ambiguous language deserves attention before the test begins. If the agreement says a vacuum function must operate, what will demonstrate that it operates as intended? Is the evidence a displayed setting, an actual reading, or a timed operating response? The appropriate method and limit should come from the agreed specification and supplier documentation rather than a generic industry number.
Separate what can be proved at the factory from what needs the installation site. A machine function may be demonstrated using the supplier’s utilities, while a requirement that depends on the plant’s power, air supply or production environment may need a clearly assigned site acceptance check.
That distinction matters across optical bonding equipment, where different control architectures call for different tests. A FAT should be written for the ordered machine, not copied from another model simply because both perform lamination.
Which Functions Must Be Demonstrated Before Shipment?
The central question during a functional demonstration is not “Does the machine run?” but “Did it respond as specified, and can we show that?” An engineer watching a press descend may see normal movement without knowing whether the selected force, position or pressure sequence was actually followed.
For a servo-controlled press, the evidence may need to distinguish force-oriented operation from displacement-controlled operation, including the specified approach behavior and cycle endpoint. A pneumatic system raises different questions: whether its agreed pressure stages occur in the correct order, how the hold is maintained and what happens during release. The control method determines the useful test, not the other way around.
Heating and vacuum deserve the same scrutiny. Where separate heating zones are ordered, each applicable zone should be checked according to the agreed method. A vacuum display showing a setpoint is not automatically proof of evacuation or hold performance at the defined condition. The report should distinguish commands, indicated values and measurements wherever the contract requires that distinction.
Recipe execution is another easily overlooked gap. A saved recipe can look correct while the machine follows an unexpected sequence. Witnessing the selected program run provides much stronger evidence than photographing its settings page. Relevant alarm responses, guarding and emergency-stop functions should also be demonstrated using approved safe test procedures—not improvised fault simulations.
For every essential function, there should be a recognizable connection between the agreed requirement, an observable machine response and the recorded result. That is the difference between a sales demonstration and equipment acceptance.
How Should Representative Samples Be Selected?
A perfectly executed test with an easy-to-handle demonstration piece can still leave the real display application unanswered. The problem is often not the panel itself but what surrounds it: a carrier that changes the loaded dimensions, a fixture that reduces clearance, or an assembly that must be handled in a particular orientation.
Representative samples should reflect the agreed panel dimensions, substrate structure, adhesive type, overall stack thickness and tooling arrangement closely enough to challenge the functions being accepted. Where several display formats are planned, the most useful selection is not necessarily the greatest number of samples. It is the smallest sensible set that covers meaningfully different loading or equipment-boundary conditions.
Consider a panel that fits the nominal pressing area but needs a carrier for support. A test without that carrier may confirm basic machine motion, yet leave the practical loading question open. That does not make the first result worthless; it means the result needs a precise scope.
Every test assembly should also remain identifiable. Sample ID, relevant material identification, fixture, selected recipe and inspection result need to belong to the same record. If a void or visual defect appears, the report should describe what was observed without automatically blaming the machine; incoming material, preparation and tooling may also influence the outcome.
FAT samples help establish whether specified equipment functions work under the agreed conditions. They do not validate the complete production process or sustained yield. For how lamination relates to the rest of the line, see the complete display bonding workflow.
If the fixture or stack is still being finalized, it makes sense to review equipment for your display project before locking the test plan. Otherwise, the FAT may approve conditions that no longer represent the assembly that will be manufactured.
What Evidence Should the FAT Report Contain?
A credible FAT report should make sense to a colleague who never visited the factory. That person needs to see not just a pass mark, but which requirement was tested, under what conditions, what the machine actually did and why the result met the agreed criterion.
The record should identify the delivered machine and specification revision, the test method, the sample or fixture involved, relevant settings, observed or measured results and the person accepting the finding. Photographs and video can be useful, especially for remote witnesses, but their value depends on showing the right machine, test condition and response. A touchscreen image that captures a setpoint is supporting context—not necessarily proof that the physical process reached it.
For tests that rely on measured values or programmable controls, identify the measuring instrument and its calibration status, along with the relevant PLC, HMI or recipe revision where applicable. If sample quality is part of the agreed acceptance criteria, link each result to the inspection method and recorded observations—for example, alignment, trapped air, surface condition or edge quality. This helps distinguish a measured acceptance result from a general visual impression.
The connection the acceptance record must preserve
Agreed requirement → test condition and sample → observed or measured response → pass, fail or documented exception
This is also where display bonding equipment configurations stop being interchangeable on paper. Two presses may both execute lamination cycles while requiring fundamentally different FAT evidence. The following JiuTu models illustrate the distinction; they are references for acceptance planning, not claims of universal material compatibility.
Evidence for servo-controlled pressing
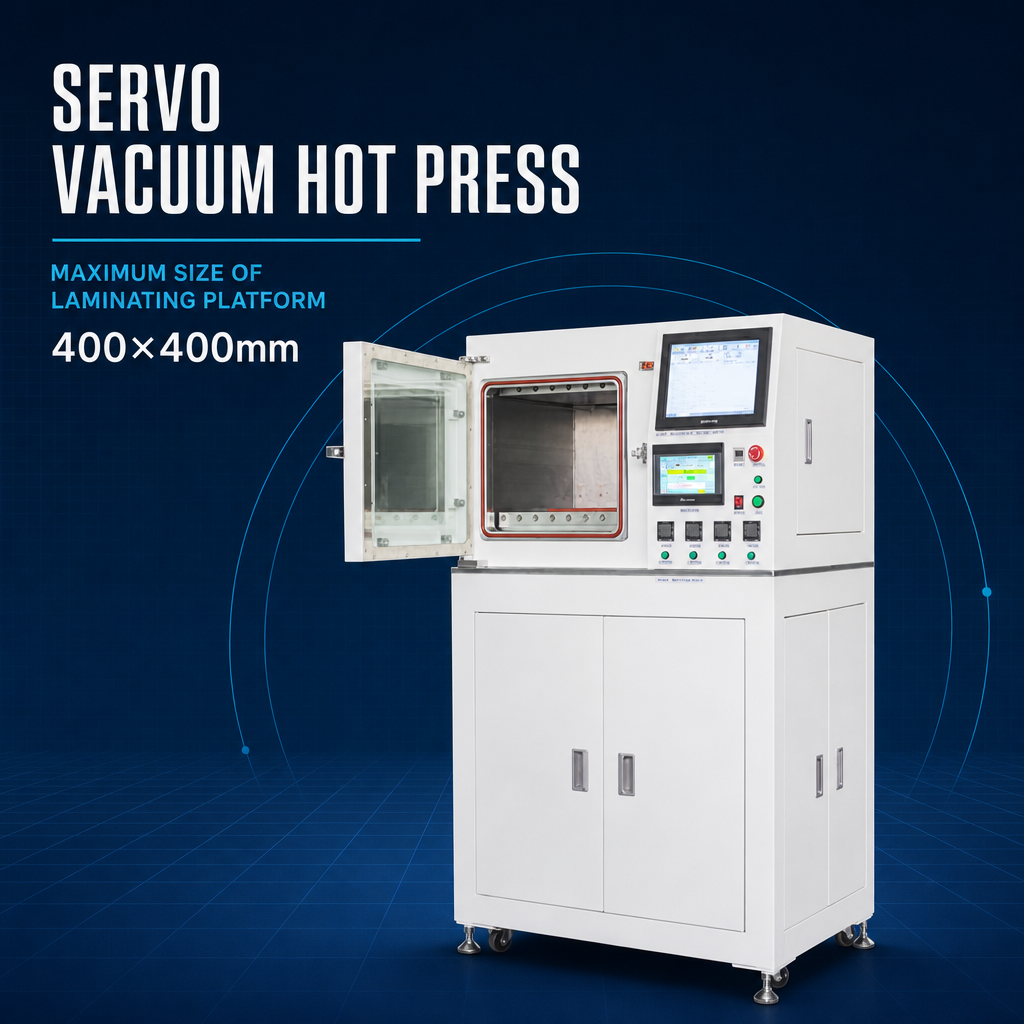
400×400-2T Servo Laminating Machine
The published 9TU-M040E configuration offers pressure and displacement modes alongside independently controlled heating and selectable chamber operation. For an order using those functions, FAT evidence should show how the selected control mode and motion respond—not simply that the platen travels. The delivered options and sample stack still govern the actual test criteria.
View model and control configuration →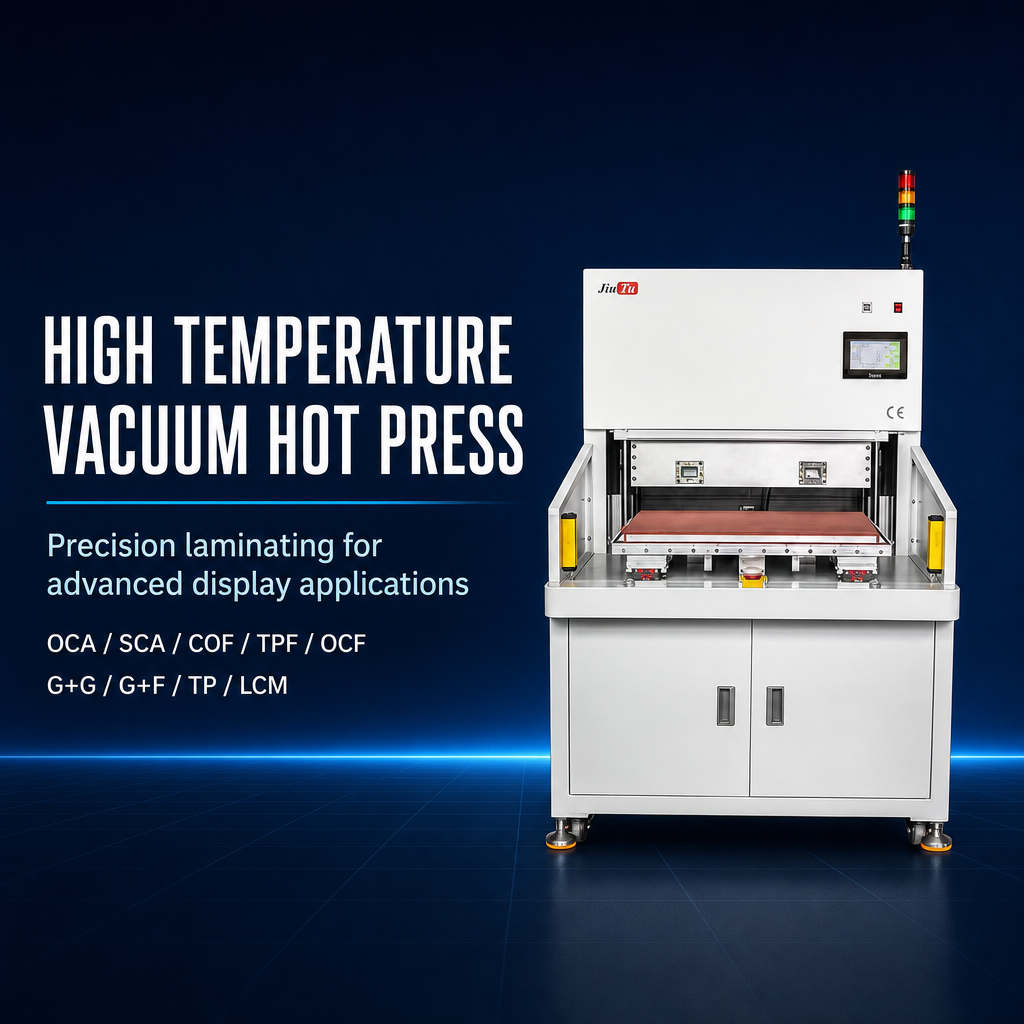
Evidence for staged pneumatic pressing
9TU-M040D Industrial Vacuum Laminating Machine
The published configuration uses pneumatic pressure with programmable stages and recipe settings. Here, the revealing FAT evidence is whether the agreed stages, timing and vacuum selections execute as intended. A servo-style movement test cannot replace verification of the pneumatic sequence, and material suitability remains subject to representative-sample review.
View model and recipe configuration →The practical lesson is not that one machine is preferable. It is that the FAT report must describe the functions actually purchased and demonstrated. A generic “lamination passed” entry leaves too much uncertainty about what was accepted.
How Are Open Items Closed Before Dispatch?
The most difficult acceptance conversation often comes after the demonstration: a function has not passed, a measurement is missing, or an agreed sample was unavailable. The temptation is to sign the report and settle the detail later. That may be reasonable for a clearly nonblocking documentation issue, but not for a failed essential function or required safeguard.
Keep one shared punch list that explains the deviation, who owns it, how closure will be demonstrated and whether it prevents shipment. A supplier’s statement that a problem has been corrected is not equivalent to a verified retest. Changes to software, controls or mechanical settings may also affect other accepted functions, so the engineer should decide whether related demonstrations need repeating.
The release decision has three possible outcomes: accepted when the agreed factory requirements have been met; conditionally accepted only for expressly authorized nonblocking items; or held when essential requirements remain unresolved. Any deferred site verification must have a named responsibility and a documented closure condition.
Before dispatch, the final acceptance record should identify the exact machine, specification revision, tested configuration, signed results and remaining obligations. If the team cannot explain what the signature covers, the acceptance scope is not yet clear enough.
Frequently Asked Questions
Can remote FAT replace an on-site visit?
It can when the parties agree that live observation, recordings and traceable measurements provide sufficient evidence. Remote viewing may limit independent inspection of mechanical details or protective functions, so any required in-person or site checks should be identified before acceptance.
What happens when samples are unavailable?
Equipment-only functions may still be demonstrated using agreed test arrangements. A criterion that depends on the actual display stack should remain unverified unless the parties approve an alternative that genuinely proves the same requirement. Record the gap and the planned follow-up test.
How should unresolved FAT items be recorded?
Give each item a unique reference, the affected requirement, observed deviation, responsible party, required corrective action and closure evidence. The acceptance record should clearly state whether the item blocks dispatch, is conditionally deferred or has passed a documented retest.
The right question at the end of an optical bonding machine FAT is not whether the factory demonstration looked successful. It is whether the evidence supports releasing this particular configuration for shipment, with the agreed samples and acceptance boundaries understood by both sides.
Define those boundaries before the visit, compare functional evidence against the specification and close the consequential findings before signing. Factory acceptance can establish shipment readiness; it cannot, on its own, guarantee compatibility with every adhesive stack or prove stable results in routine production.
For a broader view of available systems, browse JiuTu equipment options. For a live project, the more valuable next step is to agree on what the ordered machine must demonstrate.