A bubble remover machine does not need every shelf packed to run a useful batch. Start with the displays you need to process, choose trays that support them without pressing on delicate edges or flexible circuits, and give each tray a clear shelf position. A simple loading map helps the next operator repeat the same setup.
This matters when one product is a flat glass panel and another has a connector extending past its edge. Both may fit on the same shelf, but they may need different trays or even different process batches. The goal is a layout that protects the parts, is easy to handle and gives production a realistic batch count—not simply the fullest chamber.
Map the Batch Before Filling the Shelves
Imagine two displays coming off the lamination line. One is a rigid glass assembly; the other has a flexible circuit extending past one edge. They may be almost the same size, but a tray that supports the first could press on a delicate part of the second. That is why counting empty shelf positions is not the best place to start.
Look at what the line actually produces. Can these displays share the same approved pressure-and-temperature process? Do they need different supports? If the answer changes from one product to another, they may need separate loads even when there is space left in the chamber.
Draw the rack from the operator’s point of view. Number the shelves, mark the front and back, and show where each tray belongs. Include any positions that need to stay empty. Someone on the next shift should be able to follow the drawing without asking where to put a panel.
Space is not the same as usable capacity: a tray may fit on a shelf but still be unsuitable for the display sitting on it. Count only positions that have been checked for that display and its support. Some positions may need to stay empty.
This is useful when comparing bubble removal autoclaves, too. Instead of asking how many loose panels might fit, check whether the machine can accommodate your actual trays, supports and clearances.
Which Orientation Keeps Parts Supported?
Laying a flat display horizontally may seem like the obvious choice, but the tray still has to support it evenly. If a large panel rests on just a few uneven points, it may rock or bend. A curved display can be harder to support because a flat tray may touch only a few areas.
Look closely at what the tray actually touches. Frames, adhesive-sensitive edges and exposed flexible circuits should not end up carrying the panel’s weight unless the display design specifically allows it.
Can the operator load and remove it easily?
Standing panels upright or at an angle may appear to save space, but it only makes sense with a suitable fixture and a setup verified for that display. Think about the operator, too: can a loaded tray reach its shelf and come back out without touching other parts?
A tray can fit inside the chamber and still be awkward to use. Check both the space needed to move the tray safely and the clearances required by the machine manufacturer.
If you are unsure whether a large display and its fixture will fit through the door, see the guide to autoclave chamber sizing considerations. For everyday loading, concentrate on steady support and easy access to each tray.
How Should Trays Separate Different Assemblies?
Two trays can look almost identical but do different jobs. A tray determines where the display is supported, which way it faces and how close it sits to the next part.
For example, one display may be glass-to-glass, while another has a fragile module edge or a connector that sticks out. Using the same tray for both is reasonable only if it supports each one without pressing on vulnerable areas. Matching dimensions also do not mean the displays can share the same pressure-and-temperature cycle.
When a line handles several display types, clearly labelled trays or a controlled tray changeover may work better than a one-size-fits-all carrier. Operators can see which tray belongs to which product, and it is easier to keep unprocessed and finished batches apart.
Think about the loading bench, too
A tray may sit properly in the machine but still cause trouble at the loading bench. Residue can build up, supports can become damaged, and a panel can move when someone lifts the tray beside it. Inspect and clean trays using methods suitable for the tray materials and the display maker’s requirements.
Do not assume a solid tray can simply cover an existing shelf. Check the machine’s specified gas paths and loading clearances before changing the arrangement or blocking openings.
Before choosing a configuration: if your displays need different tray supports, discuss the rack layout first. You can share drawings through JiuTu’s application inquiry page so the proposed trays can be reviewed alongside the equipment.
Make the Loading Map Easy to Follow
A loading map proves its value at shift change. “Put the large panels near the back” is easy to interpret differently. A clear position label lets the next operator know exactly where the tray belongs.
You do not need a complicated record. Note which version of the map is in use, the shelf and tray position, the product or batch, which way it faces, and the approved process record. Mark positions that must stay empty so nobody tries to fill them later.
“Shelf 2 / Tray B / Front-left” is useful only when everyone agrees where the front is. Keep the same viewing direction and position names on the rack, in the drawing and in inspection records.
Try this handover check: could someone on the next shift build the same load from the map, including the empty spaces? If not, the map needs more detail.
Position records also help when something goes wrong. If edge defects keep appearing on panels from one tray position, check the support, handling and process conditions there. The location gives you a clue, not proof of the cause; confirm it with controlled checks.
Test the Loading Pattern Before Planning Output
A useful loading trial should look like a normal production run, not one sample sitting alone in an empty chamber. Use the trays you plan to run, representative displays and the intended number of occupied positions. Pay attention to loading and unloading, not just how neatly everything fits inside.
Can operators insert and remove each tray without touching neighboring parts? After processing, inspect the displays against the factory’s acceptance criteria and keep the results linked to their shelf and tray positions. If the same issue appears repeatedly in one spot, investigate it instead of hiding it in the batch average.
Once the layout is approved, the verified number of displays per batch gives you a starting point for capacity planning. Good output is a separate question: it also depends on measured yield and the time spent loading, processing, unloading and changing batches. Another shelf only helps if the extra load can be supported, processed and handled reliably.
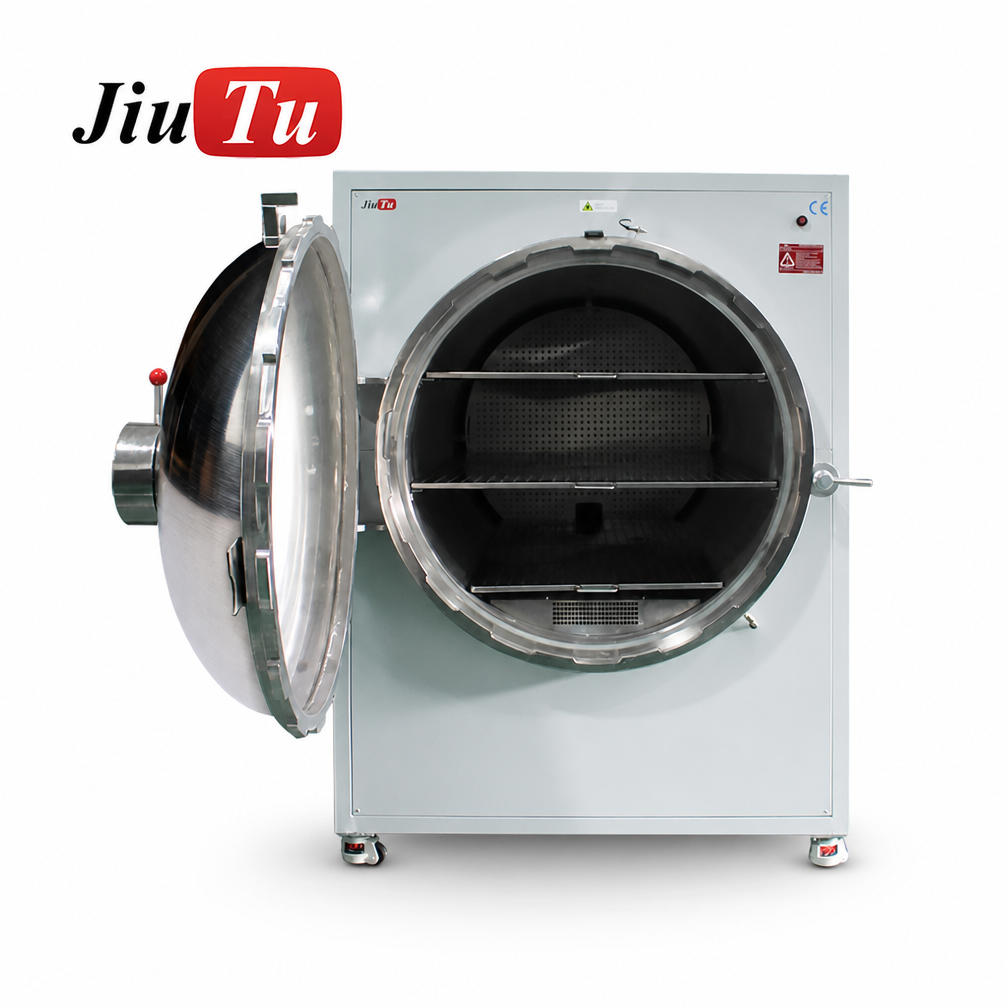
1000 × 1600 Stainless Steel Bubble Remover Machine
The 1000 × 1600 model is worth reviewing when you need several shelf levels or room for larger displays. Its product page shows perforated shelves that can be removed and repositioned.
That flexibility helps with layout planning, but it does not guarantee that your trays, display stack or adhesive process will be suitable. Share the proposed loading map when discussing the configuration.
View Product & Shelf Arrangement ↗More trays do not always mean more output. If switching between display types takes too long, or if batches cannot be tracked from lamination through bubble removal and inspection, the extra shelf space may not help production.
Before making the layout standard, make sure each display is properly supported, inspected samples meet the existing acceptance criteria, and another operator can repeat the same load. The trial does not replace approved pressure, temperature, time or material limits; those still need supplier guidance and process validation.
When asking about a machine, send the display dimensions and stack details, proposed tray and shelf positions, typical product mix and expected daily output. That tells the supplier much more than chamber size alone.
Frequently Asked Questions
Can different display stacks share a batch?
Yes, but only if their tray supports and approved processing conditions are compatible. Similar dimensions are not enough. Keep each product and batch clearly identified.
How should shelf positions be recorded?
Label each shelf and tray position, show which way the rack is viewed, and note the map revision. Link the positions to the product and batch records so inspection results can be traced back to the load.
When should a loading arrangement be revalidated?
Review the layout if you change the display stack, trays, shelf positions, orientation or handling method. Changes that could affect support or clearance may need new sample checks under the site’s change-control process.
A good loading map should make sense to someone who did not create it. It shows where each tray belongs, which positions stay empty and how the displays are supported. Once a realistic trial confirms the arrangement, the same map can guide day-to-day loading.
For production planning, use the approved loading pattern and measured results rather than the number of shelves that happen to fit inside the chamber.